Zinc-Tin Alloy Coated Self-Drilling Roofing Screws — Class 4 Corrosion Protection
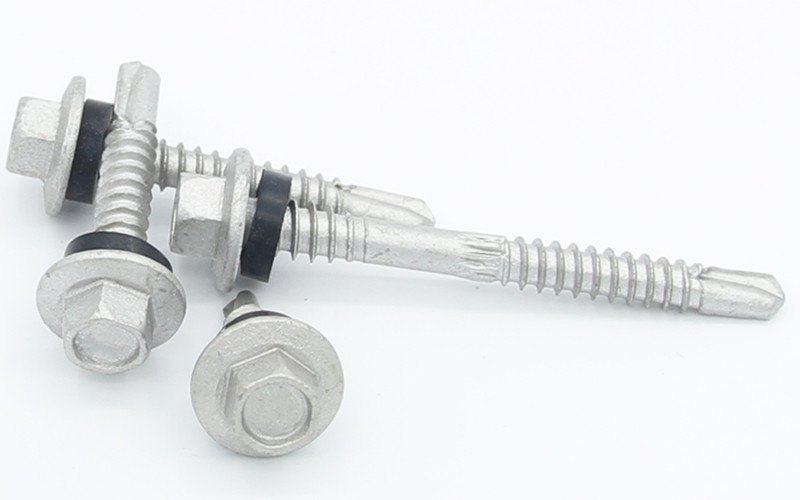
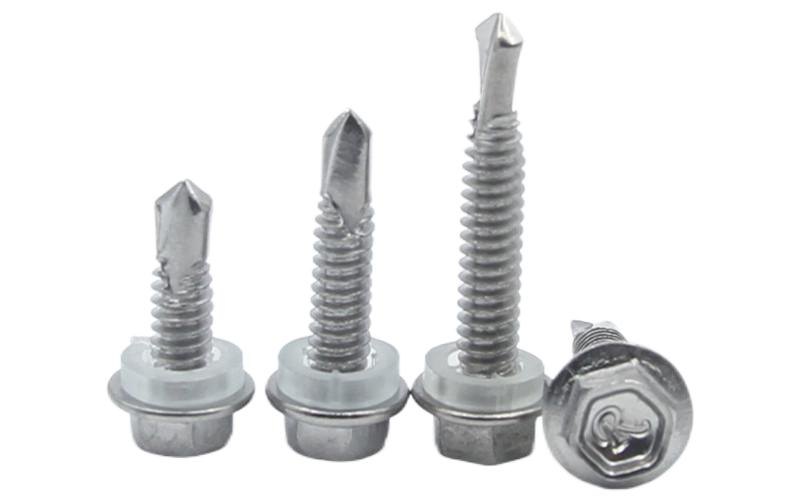
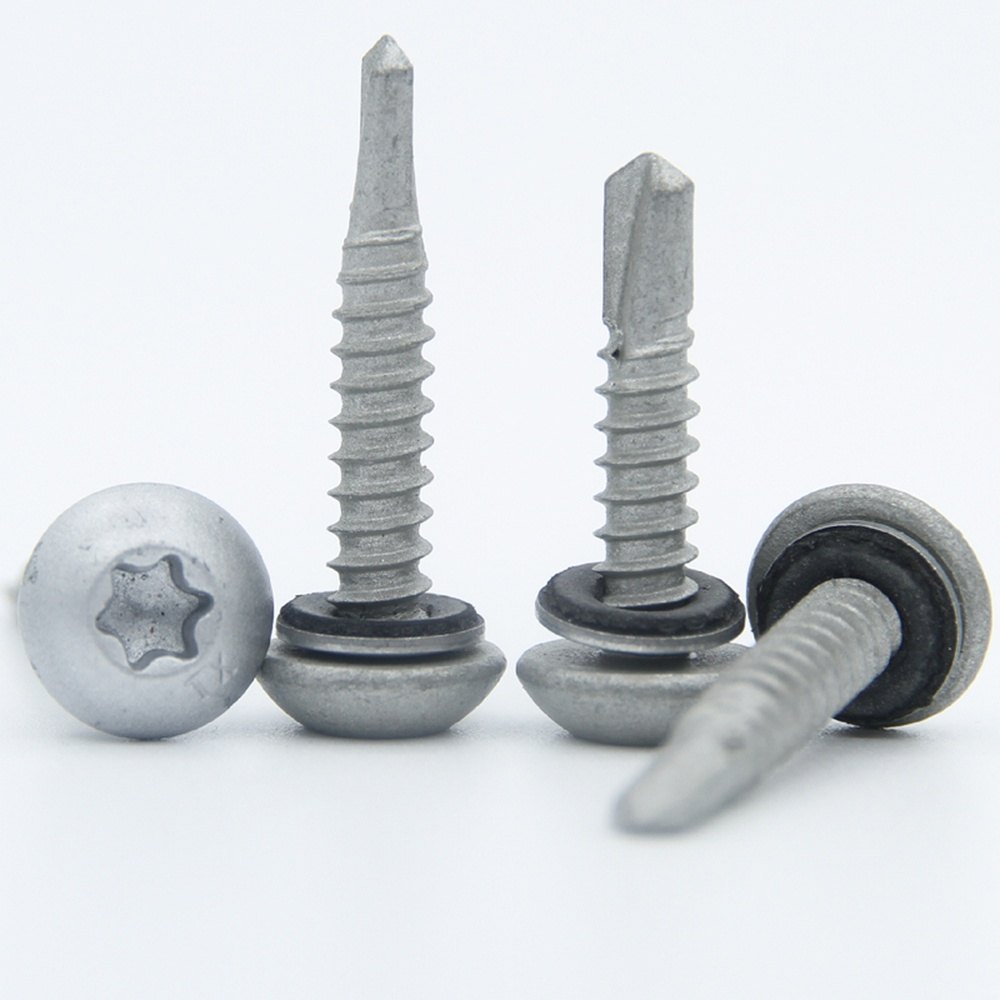
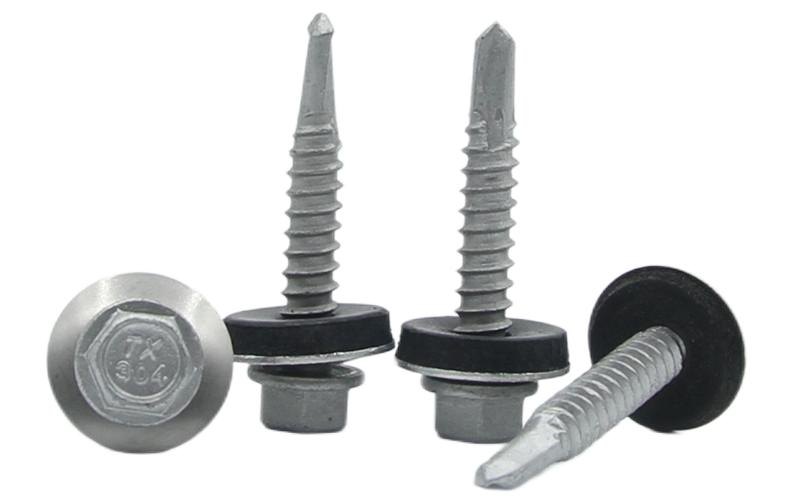
The zinc-tin alloy coated self-drilling screw is engineered for metal roofing that has to survive humid, coastal and industrial atmospheres. A mechanically plated zinc-tin layer over the case-hardened core offers several times the salt-spray life of ordinary zinc plating, while the self-drilling point installs steel-to-steel in one shot — no pre-drilling, no waiting.
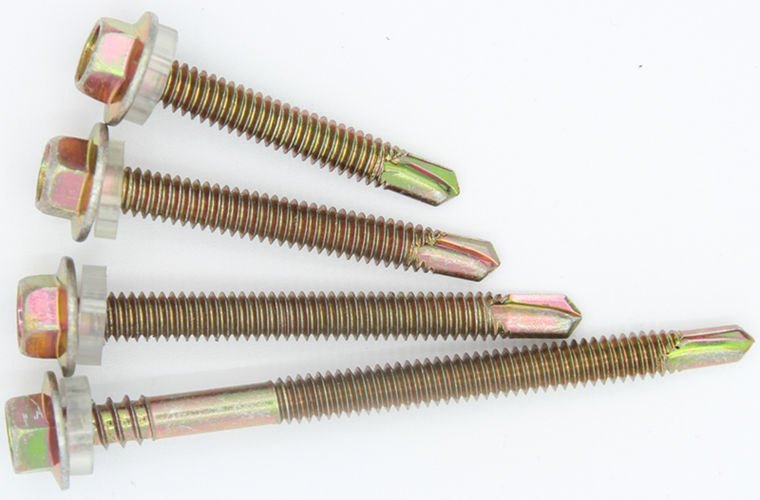
Features and Benefits
- Zinc sacrificially protects exposed steel; tin densifies the layer against white rust and edge attack
- Mechanically plated at room temperature — no acid pickling, zero hydrogen embrittlement
- Class 4 corrosion performance with 1,500 h salt spray and 25-cycle Kesternich acid rain testing
- Drill points No. 1 to No. 5 cover total steel thicknesses from 1.0 to 12.0 mm
- Bonded EPDM washer completes the weather seal at the drive point
How the Zinc-Tin Coating Protects the Fastener
Zinc provides sacrificial protection; tin refines the layer, making it denser and far more resistant to white rust and galvanic attack against aluminum or aluzinc panels. The result is a coating that stays intact under the washer, at the cut edge of the drill point and in the drilled hole itself — exactly where ordinary zinc fails first.
Typical Applications
- Aluminum and aluzinc roofing and cladding
- Coastal and island construction projects
- Agricultural buildings and livestock houses
- Industrial plants with humid or chemical atmospheres
- Long-life roofing systems with 20+ year warranties
Model Specifications
| Diameter | Threads per Inch | Drill Point | Total Steel Thickness | Length Range |
|---|---|---|---|---|
| 4.8 mm | 14 / 16 / 24 | No. 1-No. 5 | 1.0-12.0 mm | 16-220 mm |
| 5.5 mm | 14 / 16 / 24 | No. 1-No. 5 | 1.0-12.0 mm | 16-220 mm |
| 6.3 mm | 14 / 16 / 24 | No. 1-No. 5 | 1.0-12.0 mm | 16-220 mm |
| 7.0 mm | 14 / 16 | No. 3-No. 5 | 3.0-12.0 mm | 25-220 mm |
Coating System
| Layer | Thickness | Function |
|---|---|---|
| Zinc-tin alloy base | 45 μm, mechanically plated 360° | Sacrificial corrosion protection |
| Aluminum epoxy polymer top | 15 μm, dip-applied, heat cured | Barrier layer, UV and abrasion resistance |
Installation Guidelines
- Select the drill point so it clears the full steel stack before threading begins — check the capacity table.
- Drive at 0-2,500 rpm with consistent end pressure; do not push the point through faster than it can cut.
- Seat the EPDM washer to a visible compression ring — under-driving leaks, over-driving splits the seal.
- Leave min. three threads beyond the steel for rated pull-out.
- Store in dry conditions and keep the original packaging until use to protect the coating.
Why Source from BuildFastener
Coating thickness, uniformity and adhesion are checked on every production lot, and drill capacity is sampled per point size. We ship with test reports, clear head markings and export-grade packaging. Contact us for project pricing and coating-life recommendations for your site's corrosion category.
Interested in this product?
طلب عرض سعر لهذا المنتج